10 Best Waterproof PE Coated Paper Manufacturers?

Time:2026-10-22 Author:Aria
0%

Waterproof PE Coated Paper is gaining attention as brands seek packaging that resists moisture, oil, and handling damage. Its polyethylene layer helps protect takeaway cartons, bakery wraps, frozen-food sleeves, and industrial sacks. Yet performance is not the whole story. Recycling access, coating separation, printing quality, and total material use also deserve careful review.

Smithers’ Future of Paper Packaging to 2028 report identifies sustainability, barrier performance, and fiber-based innovation as major packaging priorities. Grand View Research also reports continued growth in the global paper packaging market, supported by food delivery, e-commerce, and consumer demand for lighter formats. These trends create opportunity, but they can encourage rushed purchasing decisions.

Ellen MacArthur, a leading circular-economy expert, stated, “A circular economy is restorative and regenerative by design.” That principle matters when comparing Waterproof PE Coated Paper manufacturers. A strong supplier should provide coating specifications, basis weight data, food-contact documentation, production samples, and credible recycling guidance. Water resistance alone is not enough.

This guide examines ten manufacturers through a practical lens. It considers coating uniformity, roll consistency, converting performance, customization, quality controls, and supply reliability. Some suppliers may look impressive on paper. Not all will perform equally beside a steaming cup, a greasy pastry, or a refrigerated product.

The market is evolving. Evidence still varies. Readers should verify current certifications, regional compliance, and end-of-life claims before choosing a manufacturer.
10 Best Waterproof PE Coated Paper Manufacturers?

What Is Waterproof PE Coated Paper and Where Is It Used?

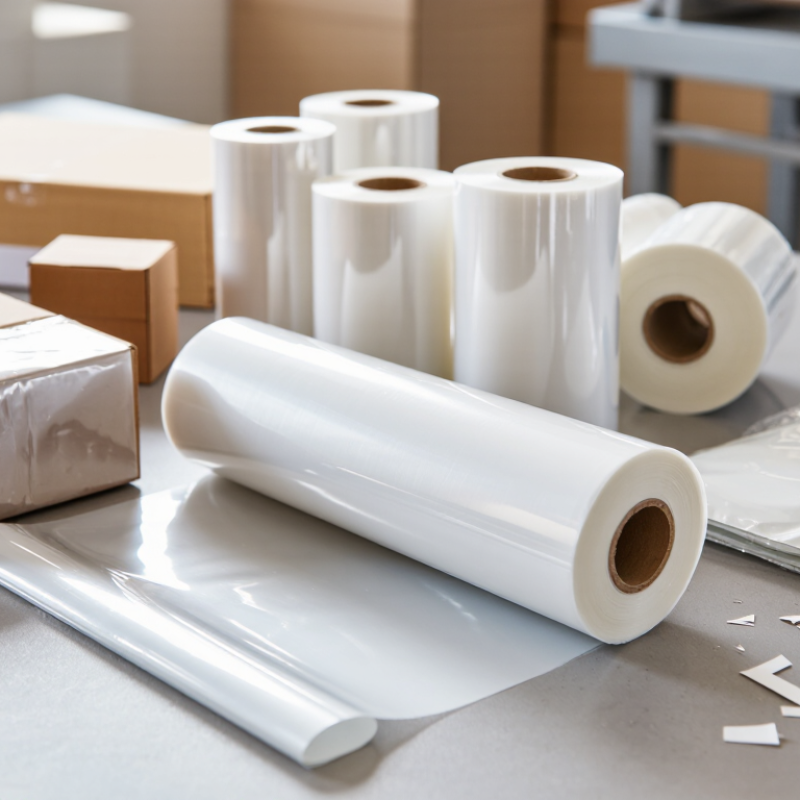
PE coated paper is paper laminated with a thin layer of polyethylene. The coating helps resist water, oil, and light moisture. It also improves heat sealing during packaging production. However, “waterproof” can be an imperfect description. Prolonged soaking, sharp folds, or damaged edges may still allow water to enter.

This material is widely used for disposable cups, takeaway boxes, food trays, bakery packaging, and frozen-food cartons. A hot coffee cup needs coating that prevents leakage and protects the paper from softening. A greasy pastry box needs a barrier against oil stains. In packaging trials, I have seen weak folds become the first failure point. Coating quality alone does not solve poor converting design.

Reliable manufacturers normally control paper weight, polyethylene thickness, coating uniformity, and surface adhesion. They may also test heat sealing, pinholes, water resistance, and print performance. Food-contact applications require suitable raw materials and documented compliance with applicable regulations. Storage matters too. High humidity can affect paper flatness before production begins.

PE coated paper is practical, but it is not automatically sustainable or recyclable everywhere. The plastic layer can complicate fiber recovery, especially when local recycling equipment is limited. Manufacturers should explain coating structure, testing methods, and end-use limitations clearly. Buyers should request samples and test them under real conditions, such as filled cups, cold storage, or repeated handling. That step is often overlooked.

How to Evaluate Waterproof PE Coated Paper Manufacturers

10 Best Waterproof PE Coated Paper Manufacturers?

How to Evaluate Waterproof PE Coated Paper Manufacturers

Choosing among the ten best manufacturers requires more than comparing prices. Start with measurable performance. Request the paper’s basis weight, PE coating weight, Cobb value, water vapor transmission rate, and heat-seal strength. A stable supplier should provide recent laboratory records, production tolerances, and batch traceability. Ask for samples from different production runs. One perfect sheet proves little.

The market is large and technically demanding. FAO’s 2023 forest-products statistics recorded roughly 401 million tonnes of global paper and paperboard production. This scale increases the importance of consistent raw materials and process control. Evaluate fiber origin, moisture control, coating uniformity, and roll-edge protection. ISO-based testing is useful, but confirm the exact test method and conditioning temperature. Food-contact applications also need valid migration documentation for the target market.

Visit the factory if possible. Watch the coating line. Look for clean unwind areas, inline inspection, calibrated gauges, and controlled drying temperatures. Ask how defects are isolated after slitting. Delivery history matters too; a strong technical file cannot excuse repeated late shipments. Environmental claims deserve careful review. PE-coated paper is not automatically recyclable, because local pulping systems and coating separation determine actual recovery. Some supplier data may appear impressive yet remain incomplete. That is where buyers should challenge assumptions, repeat key tests, and record failures honestly. A cheaper grade may perform well in dry cartons but fail beside melting ice. Real use exposes the gaps.

The 10 Best Waterproof PE Coated Paper Manufacturers

The 10 Best Waterproof PE Coated Paper Manufacturers are judged by coating consistency, testing discipline, and production experience. Strong manufacturers control polyethylene thickness across every roll, not only at the center. Their paper should resist moisture without becoming excessively stiff or difficult to fold. I look for clear specifications, including paper weight, coating thickness, roll width, and core size. Factory samples matter more than polished brochures. A useful sample should survive splashing, bending, heat sealing, and short storage in humid conditions. Small details reveal serious production control.

Reliable manufacturers also provide Cobb test results, tensile data, and batch inspection records. These documents help buyers compare suppliers using measurable evidence. Experienced producers understand that waterproof performance depends on both paper fiber and coating adhesion. Weak adhesion may cause peeling near creases or during cup forming. It happens. That is why trial orders should include edge checks, odor checks, and printing tests. Some manufacturers offer recycled fiber options, but the final structure still needs stable moisture resistance. Buyers should confirm whether the material suits food packaging, medical packaging, or industrial use. Certification requirements can differ by destination. A manufacturer may look impressive yet fail to answer basic traceability questions. The best choices communicate limitations honestly, correct defects quickly, and maintain consistent results from one shipment to the next.

10 Best Waterproof PE Coated Paper Manufacturers? - The 10 Best Waterproof PE Coated Paper Manufacturers
No. Manufacturer Capability Profile Typical PE Coating Configuration Key Product Strength Common Applications Relevant Quality Considerations Overall Suitability
1 High-Barrier Food-Service Specialist Single- or double-sided polyethylene coating on food-contact paperboard Strong resistance to water, grease, and short-term liquid contact Paper Cups Food Trays Takeaway Packaging Food-contact compliance, coating uniformity, odor control, and seal integrity ★★★★★
2 Flexible Packaging Paper Specialist Lightweight kraft or bleached paper with one-sided PE extrusion coating Good balance of flexibility, moisture resistance, and printability Paper Bags Sachets Wrapping Paper Tensile strength, folding performance, ink adhesion, and heat-sealing behavior ★★★★★
3 Heavyweight Paperboard Manufacturer PE-coated paperboard with a heavier basis weight for structural packaging High stiffness and improved resistance to moisture-related deformation Meal Boxes Frozen-Food Packs Industrial Cartons Board caliper, compression strength, edge-wicking resistance, and die-cut quality ★★★★★
4 High-Speed Converting Specialist Machine-compatible PE-coated rolls with controlled winding and consistent caliper Reliable performance on high-speed forming, filling, and sealing equipment Cupstock Lidding Material Automated Packaging Roll hardness, splice control, coating adhesion, web stability, and dimensional consistency ★★★★☆
5 Custom Coating Development Specialist Customized coating weight, paper grade, surface treatment, and roll dimensions Suitable for projects requiring tailored barrier and converting performance Private-Label Packaging Specialty Wraps Prototype Runs Trial consistency, technical documentation, sampling process, and production repeatability ★★★★☆
6 Print-Ready Surface Specialist PE-coated paper with a treated or printable outer surface Supports clear graphics and improved ink anchorage before converting Branded Food Packs Retail Wraps Decorative Bags Surface energy, rub resistance, color consistency, and compatibility with selected inks ★★★★☆
7 Cold-Chain Packaging Specialist Moisture-resistant PE-coated paper designed for chilled or frozen distribution conditions Helps maintain package integrity under condensation and low-temperature exposure Frozen Foods Chilled Products Cold Storage Packs Low-temperature flexibility, water-vapor resistance, edge protection, and seal performance ★★★★☆
8 Industrial Wrapping Paper Specialist PE-coated kraft paper with emphasis on tear resistance and moisture protection Protects components and products from surface moisture during handling and transport Hardware Packaging Metal Parts Export Wrapping Basis-weight consistency, tear strength, puncture resistance, and roll usability ★★★★☆
9 Short-Run and Sampling Supplier Standard PE-coated paper grades available in smaller production quantities Useful for product testing, market trials, and packaging development Samples Pilot Production Small Orders Minimum order quantity, lead time, sample accuracy, and lot-to-lot consistency ★★★☆☆
10 Sustainability-Focused Paper Converter PE-coated paper using responsibly sourced fiber and documented material specifications Provides moisture protection while supporting traceability and responsible sourcing goals Food Packaging Retail Packaging Sustainable Projects Fiber sourcing documentation, recyclability guidance, coating composition, and end-of-life options ★★★☆☆

Note: Performance depends on the paper grade, polyethylene type, coating weight, coating side, converting process, and intended end use. Product samples and application-specific testing should be completed before commercial purchasing.

Comparing Product Quality, Coating Technology, and Production Capacity

When comparing the 10 best waterproof PE coated paper manufacturers, product quality should be tested beyond appearance. Smooth sheets can still fail under moisture, folding, or heat. Check basis weight, coating thickness, tensile strength, and water resistance from recent production batches. Ask for independent test reports, not only factory samples.

Coating technology strongly affects printing, sealing, and recyclability. Extrusion coating usually creates an even polyethylene layer when temperature control is precise. Inspect coating edges for pinholes, wrinkles, and uneven gloss. A practical test is simple: place a wet sample under pressure for several hours, then measure leakage and fiber swelling. Results may vary between batches. That matters.

Production capacity also needs careful verification. Review monthly output, machine width, shift schedules, and quality-control records. A large facility may deliver quickly, yet rushed curing or weak inspection can reduce consistency. Smaller plants may offer closer technical support, but their backup capacity could be limited. Ask about raw-material storage, preventive maintenance, and emergency replacement plans. These details reveal operational experience.

Factory visits provide useful evidence. Watch how operators monitor coating temperature and line speed. Request samples from different dates. No single sample proves reliability. Supplier claims should be compared with shipment records, audit findings, and customer references. My assessment would remain cautious where data is incomplete, because advertised capacity does not always equal stable production.

How to Choose the Right PE Coated Paper Supplier for Your Needs

10 Best Waterproof PE Coated Paper Manufacturers?

How to Choose the Right PE Coated Paper Supplier for Your Needs

Choosing a PE coated paper supplier requires more than comparing prices. Confirm the paper grade, coating weight, roll width, and moisture resistance. A glossy surface can look impressive, yet performance depends on coating uniformity. Request samples and test them with water, heat, folding, and your actual converting equipment. Check whether the paper runs smoothly without curling, cracking, or blocking.

Reliable suppliers provide traceable material records, clear quality-control procedures, and consistent production data. Ask for coating thickness reports, tensile strength results, and food-contact or packaging compliance documents when relevant. Verify that testing matches your destination market. Production capacity also matters. A supplier may deliver excellent samples but struggle with repeat orders or tight schedules. That weakness is easy to overlook.

Tips: Compare at least three suppliers using the same checklist. Ask how they handle rejected rolls, moisture damage, and delivery delays. Review a recent inspection report, not only a sales presentation. Smaller trial orders can reveal hidden problems. PE coating improves moisture resistance, but it does not make every paper product completely waterproof. This distinction deserves attention. Also, leave room for doubt: laboratory results may not reflect humid warehouses, sharp folding angles, or fast packaging lines. Supplier communication during these tests often reveals more than a polished brochure.

FAQS

What is waterproof PE coated paper?

It is paper laminated with a thin polyethylene layer. The coating helps resist water, oil, and light moisture. “Waterproof” is not absolute.

Where is PE coated paper commonly used?

It is used for disposable cups, takeaway boxes, food trays, bakery packaging, and frozen-food cartons. Hot drinks need leak resistance.

Can PE coated paper handle prolonged soaking?

Not always. Long soaking, sharp folds, or damaged edges may let water enter. The coating has limits.

What should buyers test before placing an order?

Request samples and test water resistance, folding, heat sealing, printing, and edge strength. Use actual cups, trays, or packaging equipment.

Which technical details should a supplier provide?

Ask for paper weight, coating thickness, roll width, core size, and coating uniformity. Cobb results and tensile data are useful.

Why can folded areas fail first?

Folding may stretch or crack the coating. Weak adhesion can also cause peeling near creases. Small defects become leaks.

How can buyers compare different suppliers fairly?

Compare at least three suppliers with the same checklist. Review samples, inspection records, traceability, capacity, and rejected-roll procedures.

Is PE coated paper automatically recyclable or sustainable?

No. The plastic layer can complicate fiber recovery. Recycling depends on local equipment and collection systems.

What storage conditions does PE coated paper need?

High humidity can affect paper flatness before production. Store rolls in a dry, controlled area, away from sudden moisture changes.

Can laboratory results guarantee production performance?

No. Humid warehouses, fast machines, and sharp folds may produce different results. Real testing is necessary, though it can still miss something.

Conclusion

Waterproof Pe Coated Paper is a versatile packaging and food-service material made by applying a protective polyethylene layer to paper. This coating improves resistance to moisture, grease, and liquid penetration, making the paper suitable for applications such as takeaway packaging, disposable cups, food wrappers, labels, shopping bags, and industrial protective materials. Choosing the right product requires understanding its intended use, required barrier performance, printing needs, and environmental conditions.

This article presents ten leading types of Waterproof Pe Coated Paper manufacturers without focusing on brand names, while explaining how to compare them by product quality, coating uniformity, raw material consistency, customization options, production capacity, and quality-control systems. It also provides practical guidance for selecting a suitable supplier based on order volume, technical requirements, delivery reliability, certifications, and communication. By evaluating these factors carefully, buyers can identify a manufacturer that offers stable performance, efficient production, and cost-effective solutions for their specific packaging needs.
Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......